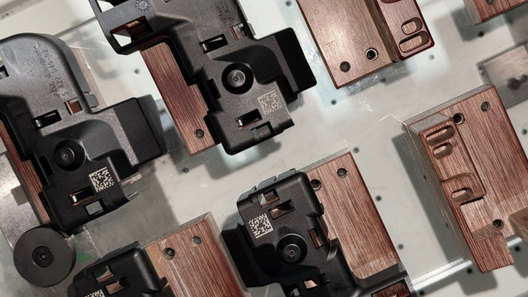
Tool transfer and process stabilisation in automotive series production
An existing partner approached us to transfer an ongoing automotive series production project as quickly as possible (ASAP), due to quality problems and failure to meet OEM requirements.
To take over an ongoing project seamlessly and establish a stable, defect-free injection moulding process for series production that meets OEM requirements for our existing customer.
Project parameters
360 000 units/year
Production volume
PA46
Material
4 cavities
Tool configuration
150 T
Injection moulding machine
100%
QR code readability inspection
IATF
Automotive compliance
Challenges
During the transfer, we had to stabilise three critical areas within a short timeframe.
QR code readability
Illegible markings rejected by the OEM on several occasions
Insufficient contrast and marking quality at the previous supplier
Recurring quality concerns during series production
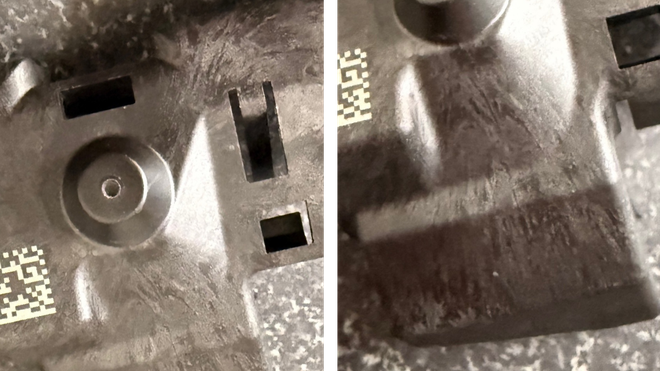
Surface discolouration
Clearly visible surface defect of approximately 3×3 cm on the injection-moulded part
Inconsistent visual quality leading to complaints
Material preparation was suspected to be the cause
Incomplete documentation
The tool was transferred with incomplete documentation
Series production parameters had to be redefined
Stable, repeatable settings were needed at short notice
We delivered a lasting solution through engineering analysis, process parameter redefinition and 100% inspection.
Mitter's solution
01 Redefining process parameters
Integrating the tool into a Netstal 150 t production environment
Establishing settings suitable for series production
Documenting critical parameters and inspection points
02 QR code marking and fixture
Introducing new laser marking parameters
Developing a positioning fixture
Introducing 100% automated readability inspection
03 Drying protocol and moisture control
Integrating a Wittmann dryer
Standard drying: 4 hours / 120°C
Stabilising moisture content below 0.02%
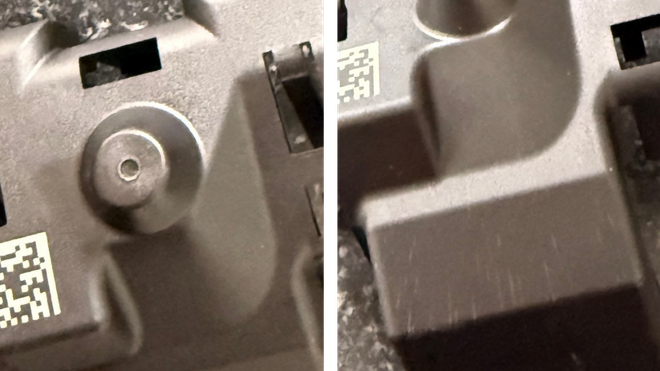
Eliminating the surface defect – before and after
The drying protocol and process stabilisation eliminated the discolouration, producing a uniform surface.
Előtte: Felületi foltosodás sorozatgyártásban
Utána: Homogén felület stabil technológiával
Customer feedback
“A great result: the QR code is much clearer, and the surfaces of the parts are also far more uniform than with the previous supplier.”
— Tier-1 partner, OEM audit
Planning a production transfer? Let's discuss the technical details.
Request a quote for toolmaking & plastic injection molding
Please enter your contact details and request – we will get in touch with you shortly.
Thank you for your interest. A member of our team will contact you within 24 hours. Further communication will be conducted in English.
Angebot für Werkzeugbau & Kunststoff-Spritzguss anfordern
Geben Sie bitte Ihre Kontaktdaten und Ihr Anliegen an – wir setzen uns zeitnah mit Ihnen in Verbindung.
Vielen Dank für Ihr Interesse. Ein Mitarbeiter unseres Unternehmens wird sich innerhalb von 24 Stunden mit Ihnen in Verbindung setzen. Die weitere Kommunikation erfolgt in englischer Sprache.