Precision manufacturing company with a multinational background
Component
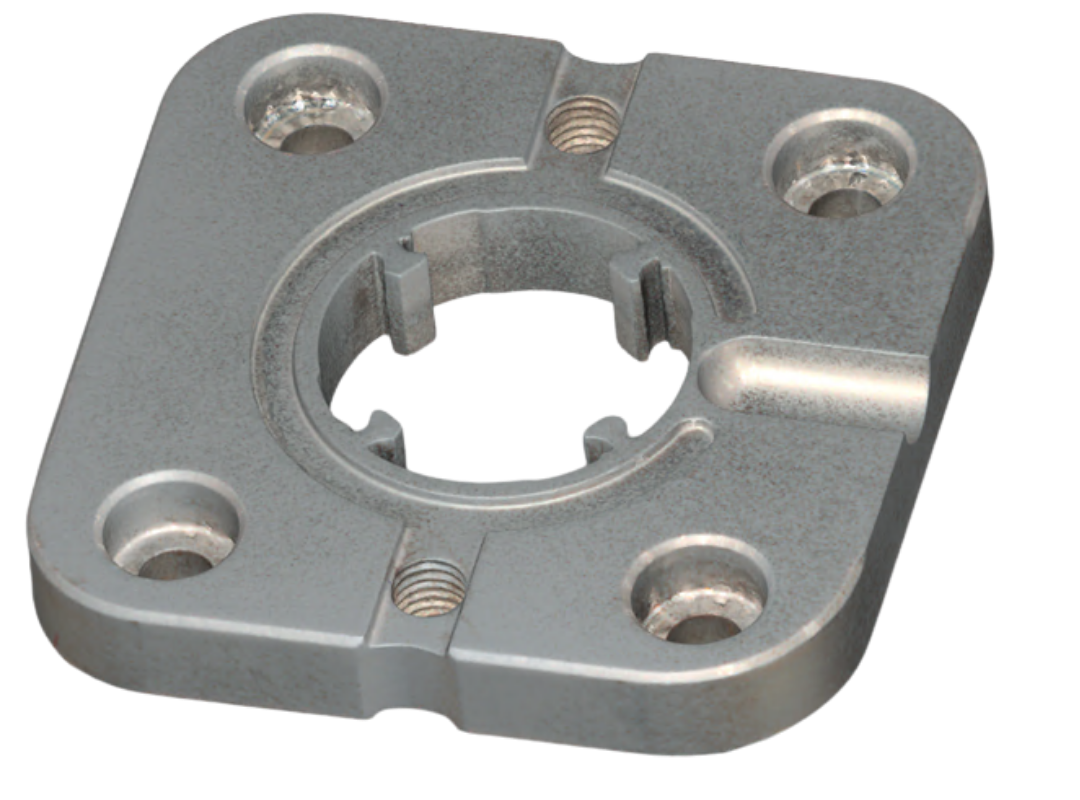
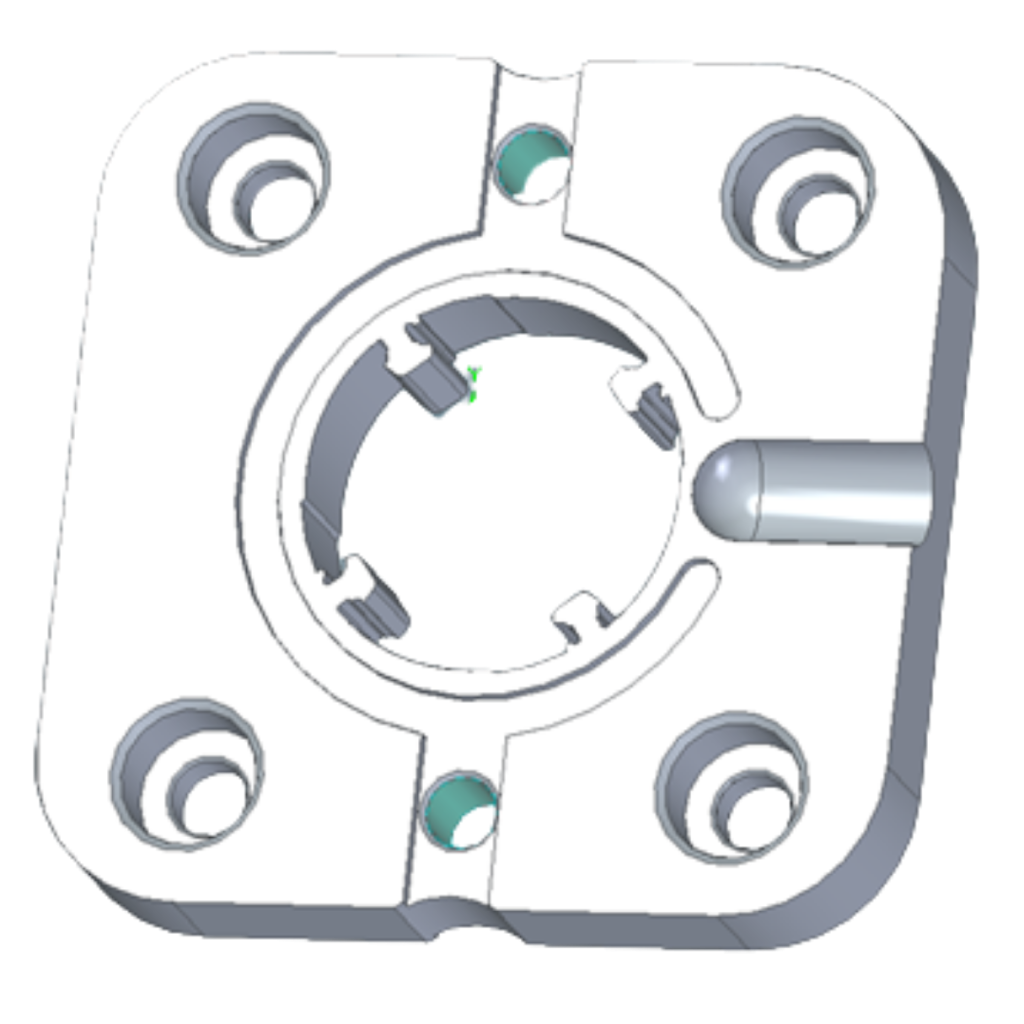
Injection-moulded stator with an iron core
Objective
Eliminate flash,
stable production
Technology
3D laser scanning and reverse engineering
The challenge: flash on the component and unstable production
Our partner approached us because flash had appeared on an injection-moulded stator component. After checking the production parameters, it became clear that the defect was caused by a worn tool insert rather than process settings.
Quality complaints and scrap
Costly rework in series production
Delivery deadlines at risk
Critical surfaces: where wear of just hundredths of a millimetre causes flash.
The engineering decision: remanufacture rather than repair
After examining the insert's condition in detail, we had two options.
Our aim was a long-term solution.
Welding and remachining
Time-consuming due to the extent of surface wear
Difficult to carry out because of the complexity of the affected surfaces
A more expensive solution for the above reasons
Recommended solution
Complete remanufacture
Stable geometry for flash-free shut-off
3D laser-scanned precision
Permanently available digital model
3D laser scanning: capturing the actual geometry
We digitised the worn insert using an industrial 3D laser scanner.
This step provided the basis for engineering certainty.
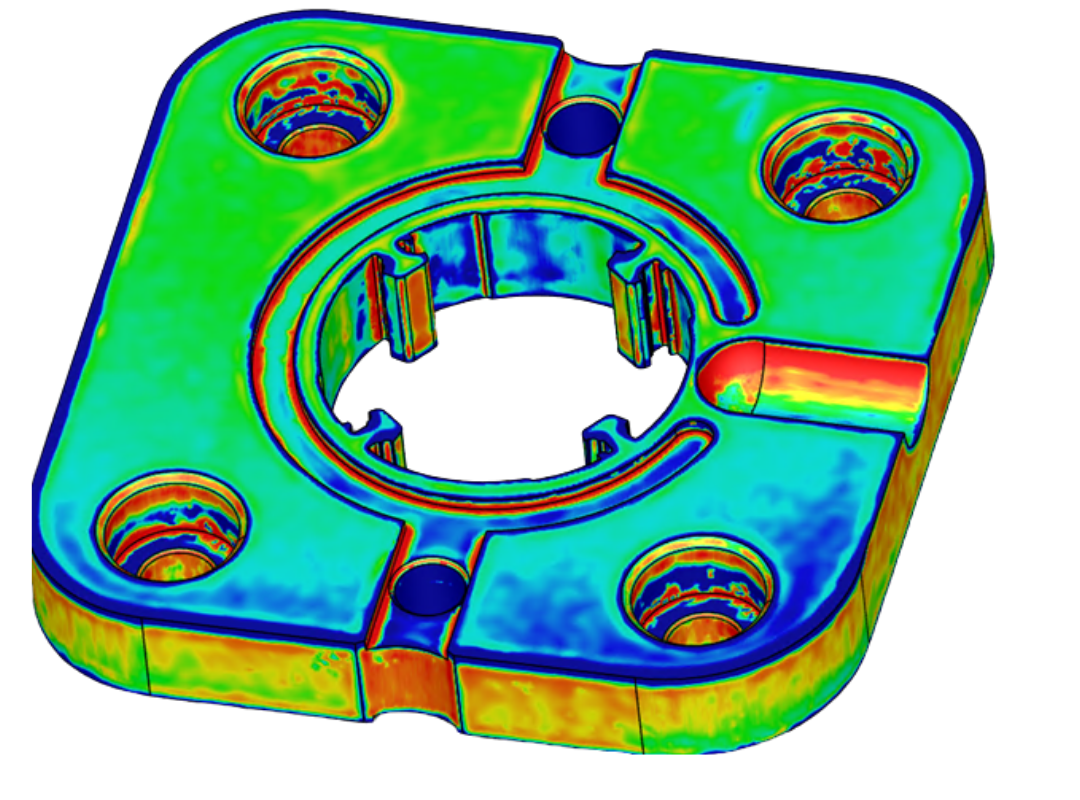
High-precision capture
Visual identification of worn surfaces
A reliable digital basis for manufacturing
Digital reverse engineering: reconstructing the missing geometry
Our engineers created reference geometry from sections in good condition, then reconstructed the complete model using a symmetrical arrangement.
The new insert was manufactured from the reconstructed model, but trial production showed that the fit of the stator's iron core required further fine-tuning.
Modification of critical surfaces
Application of precise offsets
Precision wire EDM rework
Production flexibility: zero downtime
We removed the tool insert only for the short scanning period, allowing the customer's production to continue throughout the process.
Fast scanning
We removed the faulty insert from the tool only for measurement.
Step 1
Uninterrupted series production
We returned the old insert immediately so that stator production could continue.
Step 2
Remanufacture
The new insert was manufactured in parallel using the scanned data.
Step 3
Results
Zero downtime
Reconstructed geometry
Stable series production
Digital twin
Zero downtime
Reconstructed geometry
Stable series production
Digital twin
Whether you face worn tool inserts, missing 3D documentation or recurring quality defects, our engineering team is ready to provide a solution.
Don't wait for scrap rates to rise – ask our experts to help restore your process!
Request a quote for toolmaking & plastic injection molding
Please enter your contact details and request – we will get in touch with you shortly.
Thank you for your interest. A member of our team will contact you within 24 hours. Further communication will be conducted in English.
Angebot für Werkzeugbau & Kunststoff-Spritzguss anfordern
Geben Sie bitte Ihre Kontaktdaten und Ihr Anliegen an – wir setzen uns zeitnah mit Ihnen in Verbindung.
Vielen Dank für Ihr Interesse. Ein Mitarbeiter unseres Unternehmens wird sich innerhalb von 24 Stunden mit Ihnen in Verbindung setzen. Die weitere Kommunikation erfolgt in englischer Sprache.